What Drives NDT Solutions Cost in Industrial Inspection Projects?
For procurement teams planning industrial inspection projects, understanding NDT solutions cost is essential for balancing safety, compliance, and long-term asset reliability.
Pricing varies widely with inspection method, equipment capability, automation, certification, deployment conditions, and data-analysis requirements. Buyers need a lifecycle view, not a catalog-price comparison.
The central procurement question is not simply which NDT system costs less initially. It is which solution detects relevant defects reliably at an acceptable total operating cost.
For industrial buyers, the strongest purchase decision connects inspection performance to asset risk, outage exposure, labor availability, reporting obligations, and future maintenance strategy.
Start With the Inspection Risk, Not the Equipment Price
NDT solutions cost begins with the consequence of a missed indication. A minor cosmetic defect and a fatigue crack in a pressure boundary require very different inspection investments.
Procurement teams should first define the component, material, geometry, service environment, expected damage mechanisms, and regulatory obligations before requesting equipment or service quotations.
Common damage mechanisms include weld porosity, lack of fusion, corrosion thinning, hydrogen cracking, delamination, inclusions, fatigue, creep damage, and surface-breaking defects.
Each mechanism has a preferred detection approach. Selecting a method because it appears inexpensive can create false economies when its probability of detection is inadequate.
For example, visual testing may identify accessible surface conditions, while ultrasonic testing can assess internal discontinuities without removing an asset from service for extended periods.
Radiographic testing may provide valuable permanent records for certain welds, but its cost profile includes safety controls, access limitations, and potentially longer site coordination.
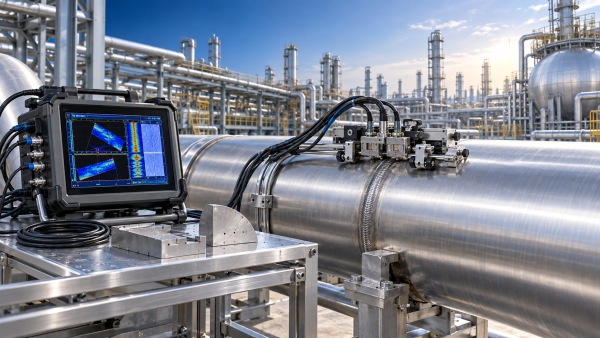
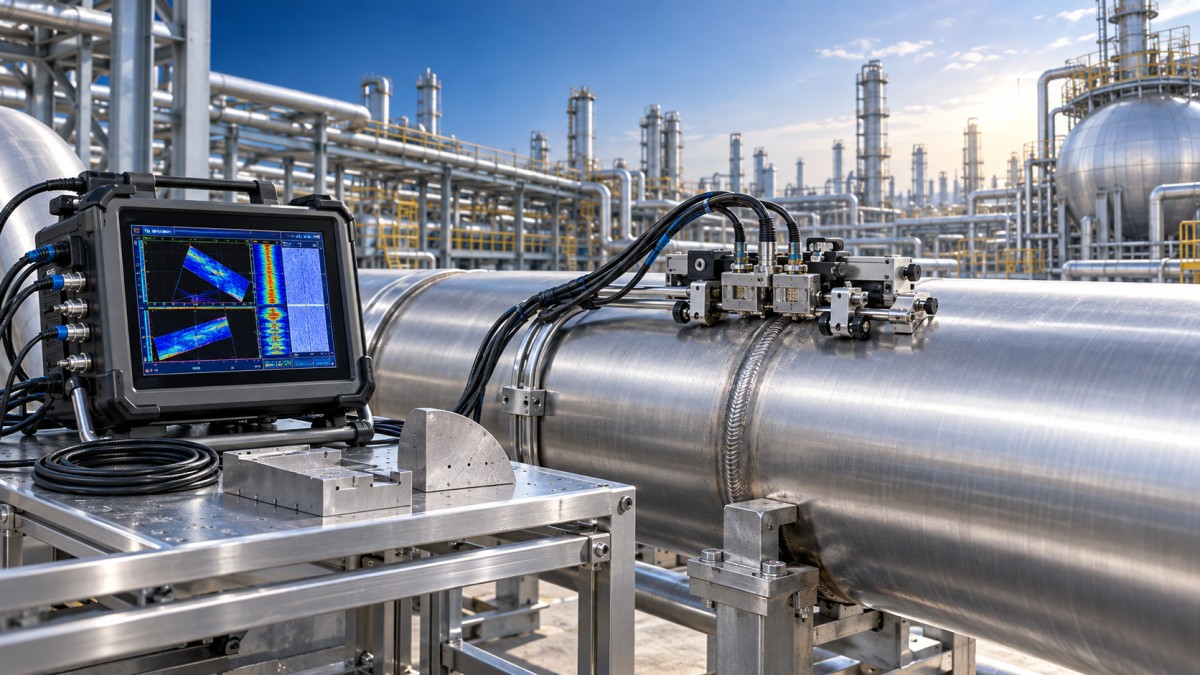
Phased array ultrasonic testing often carries a higher equipment and setup cost than conventional ultrasonics, yet can reduce scanning time and improve coverage documentation.
Industrial computed tomography delivers detailed volumetric insight for complex castings, additive parts, and assemblies, although capital, shielding, throughput, and expertise requirements are substantial.
Buyers should translate technical needs into measurable acceptance criteria. These include minimum detectable flaw size, coverage area, inspection speed, reporting format, and allowable false-call rate.
That specification prevents suppliers from quoting technically incomparable systems. It also clarifies when a premium NDT solution genuinely lowers operational risk rather than adding unnecessary capability.
How the NDT Method Changes the Cost Structure
The selected method is usually the largest direct driver of NDT solutions cost because it determines the instrument platform, consumables, operator skill, safety requirements, and workflow.
Visual testing and liquid penetrant testing generally require lower equipment investment, but preparation, cleaning, dwell time, and manual interpretation can increase recurring labor costs.
Magnetic particle testing is effective for ferromagnetic materials and near-surface defects. Its budget must include magnetization equipment, consumables, cleaning, and demagnetization where required.
Eddy current testing can inspect conductive materials quickly, especially for tubing, aircraft structures, and surface flaws. Cost depends heavily on probe design and calibration complexity.
Conventional ultrasonic testing offers a flexible middle ground for many thickness and weld inspections. However, results may depend more strongly on individual operator technique.
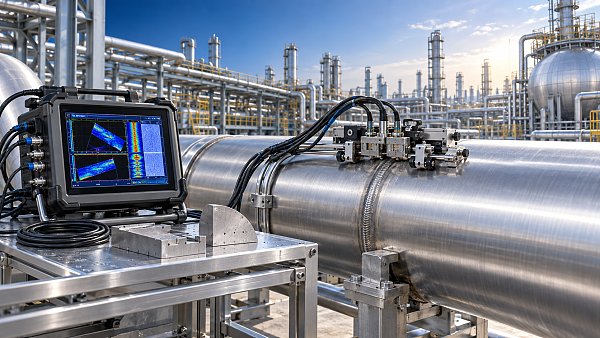
Phased array and time-of-flight diffraction systems increase hardware and software expenditure, yet provide encoded data, improved geometry handling, and more auditable inspection records.
Radiography requires consideration beyond the source or detector price. Site exclusion zones, radiation safety personnel, permits, storage, and production disruption can dominate project economics.
Digital radiography can reduce film processing and accelerate image review, but detector durability, image-quality requirements, software licensing, and cybersecurity controls affect total ownership cost.
When comparing methods, ask suppliers to separate capital costs from per-inspection costs. A lower purchase price can conceal higher labor, consumable, access, or repeat-inspection expenses.
Method selection should also consider whether inspections occur during planned shutdowns, routine production, field maintenance, or high-volume manufacturing, since utilization changes the economic result.
What Equipment Capability and Configuration Add to the Budget
Two systems described as ultrasonic or radiographic equipment can have radically different prices because their performance envelope, reliability, portability, and data capabilities differ substantially.
Frequency range, channel count, pulse energy, detector resolution, scanning area, dynamic range, and environmental protection all influence the quoted price of an inspection platform.
A basic handheld unit may be appropriate for intermittent thickness checks. A multi-axis automated scanner is justified when repeatability, traceability, and production throughput are critical.
Probe and fixture design often deserve more scrutiny than the base instrument. Complex geometries may require custom wedges, encoded scanners, reference blocks, and purpose-built handling tools.
Custom engineering raises the initial NDT solutions cost, but can reduce setup variation and operator dependence across repeated inspections of the same component family.
Procurement should distinguish standard accessories from application-specific tooling. Suppliers sometimes quote a base package that cannot perform the requested inspection without later additions.
Environmental requirements also matter. Offshore platforms, refineries, mines, foundries, and aerospace production sites may require rugged enclosures, ingress protection, temperature tolerance, or intrinsically safe designs.
Portable systems can lower access and transportation effort, while fixed systems may improve throughput and process control. The right choice depends on inspection location and annual volume.
Ask whether quoted specifications are validated on comparable materials and thicknesses. Performance claims based on ideal test samples may not transfer to rough, coated, curved, or hot surfaces.
A practical technical evaluation should include representative test pieces, expected defect types, required scan speed, and an agreed demonstration of probability of detection before final selection.
Why Automation Can Raise Initial Spend but Reduce Total Cost
Automation is one of the most visible contributors to NDT solutions cost. It includes encoded scanners, robotics, motion control, part handling, software integration, and automated decision support.
Its value is strongest where inspection volume is high, component geometry repeats, skilled labor is scarce, or manual scanning creates inconsistent coverage and documentation.
Automated systems typically require engineering work before deployment. This includes fixture design, scan-path programming, safety interlocks, validation trials, and integration with production controls.
These activities can make the first project appear expensive. Buyers should spread those nonrecurring engineering costs across expected production volume and system operating life.
In repetitive manufacturing, automation may reduce inspection cycle time, decrease rework, stabilize measurements, and create digital records that support supplier quality and root-cause analysis.
For low-volume repairs or varied field assets, a fully automated cell may be difficult to justify. Flexible portable equipment and skilled service providers can offer better economics.
Robotics should not be purchased solely to replace technicians. The business case must quantify improved access, reduced exposure, higher uptime, better coverage, or lower inspection bottlenecks.
Artificial intelligence tools can assist image classification and indication triage. Their commercial value depends on training data quality, validation, explainability, and clear human review procedures.
Request cycle-time assumptions, staffing requirements, maintenance intervals, and availability targets from automation suppliers. These inputs are necessary for a realistic total-cost model.
Also confirm who owns application software, scan recipes, inspection data, and future modification rights. Proprietary dependencies can materially affect lifecycle cost and operational flexibility.
Labor, Certification, and Compliance Often Decide Project Economics
Equipment is only one component of an inspection budget. Qualified personnel, certification requirements, procedure development, supervision, documentation, and client witnessing frequently determine project cost.
Many sectors require inspectors qualified under recognized schemes, customer specifications, national rules, or industry codes. The required level of certification affects labor rates and scheduling.
Complex methods may need experienced Level II or Level III oversight for procedure approval, technique qualification, sensitivity settings, and interpretation of ambiguous indications.
For field projects, labor costs also include travel, accommodation, site induction, security clearance, confined-space training, shift premiums, and standby time during operational delays.
Procurement teams should ask whether supplier pricing includes procedure qualification and technical authority. Omitting these items can produce a low quote followed by unavoidable change orders.
Compliance costs become especially significant in nuclear, aerospace, oil and gas, rail, power generation, and pressure-equipment applications, where traceability requirements are rigorous.
A credible supplier should identify the governing codes, required personnel qualifications, calibration controls, report retention requirements, and any third-party verification expected for the project.
Do not assume an experienced technician can substitute for a qualified procedure. A technically competent inspection can still fail an audit if documentation and approvals are incomplete.
When purchasing equipment for internal use, include recurring training, refresher certification, competency assessments, and succession planning. A system without qualified operators may remain underutilized.
Comparing labor models is useful: outsourced inspection, internal inspection, managed service, and hybrid arrangements each allocate technical risk and fixed cost differently.
Data, Software, and Reporting Requirements Add Long-Term Costs
Modern industrial inspection increasingly produces encoded scans, high-resolution images, thickness maps, and digital reports. Managing this information is now a meaningful part of NDT solutions cost.
Basic instruments may store files locally, while advanced systems require analysis workstations, secure servers, cloud storage, integration interfaces, user accounts, and software maintenance contracts.
Data requirements should match the asset strategy. For one-time screening, detailed digital-twin integration may be excessive. For critical assets, historical comparison can justify the investment.
Procurement should define who needs access to inspection results: technicians, quality engineers, maintenance planners, asset integrity teams, customers, regulators, or external auditors.
Interoperability matters when inspection data must connect with enterprise asset management, manufacturing execution, quality management, or condition-monitoring systems. Integration can require additional engineering effort.
Software licensing models vary considerably. Confirm whether licenses are perpetual, subscription-based, tied to hardware, limited by users, or subject to charges for major upgrades.
Cybersecurity should be evaluated early, especially when instruments connect to plant networks or cloud services. Security reviews can delay deployment and create unbudgeted implementation work.
Reporting templates should be reviewed before purchase. The system must produce evidence that supports acceptance decisions, repair planning, audit readiness, and customer communication without manual reformatting.
Ask suppliers about raw-data export, file-format longevity, backup options, and restoration procedures. Inspection records may be needed years after the original equipment is retired.
Good data management does not merely improve presentation. It supports trending, risk-based inspection planning, defect growth assessment, and more informed capital-maintenance decisions.
How to Compare Quotations on a Total Cost of Ownership Basis
A disciplined comparison framework helps procurement teams avoid choosing the cheapest headline quote. Evaluate each proposal against a common scope, operating profile, and risk-adjusted business case.
Start by separating one-time costs: equipment, scanners, fixtures, installation, validation, training, software setup, safety infrastructure, and procedure development should be visible line items.
Then estimate recurring costs over the expected service period. Include labor, calibration, consumables, repairs, licenses, travel, data storage, spares, and periodic recertification.
Consider indirect costs as carefully as direct costs. Production downtime, scaffolding, surface preparation, component handling, radiation exclusion zones, and reinspection can exceed instrument expense.
Model the financial effect of inspection performance. Better defect detection may prevent failures, reduce warranty exposure, avoid unplanned shutdowns, and improve confidence in repair-or-replace decisions.
For critical assets, use scenarios rather than a single estimate. Compare normal operation, a high-defect-rate case, delayed inspection access, and an unplanned outage caused by missed damage.
Supplier service coverage should be scored alongside price. Response time, local technical support, spare availability, loaner equipment, application expertise, and calibration turnaround influence operational continuity.
Request a clear statement of exclusions and assumptions. This is particularly important for access preparation, custom tooling, travel, radiation controls, operator certification, and software implementation.
A pilot inspection can be more valuable than extensive proposal presentations. It reveals setup time, data quality, throughput, ergonomic constraints, and the supplier's ability to handle real conditions.
Finally, document the decision rationale in terms that engineering, operations, finance, and quality teams can all evaluate. Alignment reduces disputes after implementation begins.
Questions Procurement Teams Should Ask Before Awarding an NDT Contract
Before awarding a contract or approving capital expenditure, buyers should confirm that the proposed technique detects the required damage mechanism on representative component conditions.
Ask what evidence supports performance claims. Relevant demonstrations, validated procedures, reference standards, probability-of-detection studies, and prior applications are more useful than generic brochures.
Confirm the complete deliverable: raw data, interpreted results, annotated images, repair recommendations, acceptance decisions, calibration certificates, and final reports may have different commercial values.
Clarify whether the supplier will provide on-site technical authority when unexpected indications appear. Escalation speed matters when inspection results affect production release or shutdown duration.
Ask how the method handles coatings, surface roughness, temperature, limited access, complex geometry, and dissimilar materials. These conditions frequently determine whether planned productivity is achievable.
Evaluate calibration and verification arrangements. A low initial price loses value quickly when recalibration requires long shipping delays, expensive service visits, or unavailable reference standards.
For automated systems, determine how recipe changes are priced and delivered. New part numbers, design revisions, and altered acceptance criteria can require costly reprogramming.
Assess vendor stability and support capacity. Long-lived industrial assets need reliable access to technical expertise, replacement probes, software updates, and archived inspection knowledge.
Contract terms should address data ownership, confidentiality, intellectual property, acceptance testing, warranty coverage, liability limits, and responsibilities for failed inspection performance.
These questions shift the evaluation from purchasing a device or service toward purchasing dependable inspection capability that remains useful throughout the asset lifecycle.
Making a Defensible NDT Investment Decision
The most effective way to manage NDT solutions cost is to match inspection capability with consequence of failure, inspection frequency, operating environment, and evidence required for compliance.
Low-cost methods remain appropriate for accessible, low-risk conditions when they meet the detection objective. Higher-cost technologies earn their place when they improve confidence, speed, or traceability.
Procurement teams should resist both extremes: under-specifying equipment that cannot answer the integrity question and over-specifying advanced systems that will not be adequately utilized.
A transparent total-cost model, supported by representative trials and clear technical acceptance criteria, gives buyers a defensible basis for comparing apparently different NDT proposals.
Ultimately, the best investment is the solution that produces reliable inspection evidence with manageable operational burden, helping the organization protect people, assets, schedules, and compliance commitments.